Call: 08071724603
 Send Inquiry

 Send Inquiry
Lobe Pump
MOQ : 1 Unit
Lobe Pump Specification
- Theory
- Rotary Lobe Pump
- Control System
- Manual/Automatic
- Discharge Pressure
- Up to 1.6 MPa
- Working Temperature
- -10C to 120C
- Head Size
- Up to 80 meters
- Inlet/Outlet
- Threaded/Flanged, various sizes
- Flow Rate
- Up to 60 m3/hr (varies by model)
- Frequency
- 50/60 Hz
- Voltage
- 220V/380V
- Caliber
- DN25 to DN100
- Mounting Type
- Base Mounted
- Max Suction
- 8 meters
- Noise Level
- <75 dB
- Speed
- Up to 960 rpm
- Features
- Hygienic Design, Easy Cleaning, CIP/SIP Capable, Non-pulsating Flow, Reversible Flow
- Material
- Stainless Steel, Cast Iron, Others (as per demand)
- Structure
- Horizontal
- Power
- 0.75 kW to 15 kW
- Standard
- ISO, CE, GMP
- Fuel Type
- Electric
- Pressure
- Up to 1.6 MPa
- Usage
- Industrial Fluid Transfer, Food Grade Pumps, Chemical, Pharmaceuticals, Dairy
- Application
- Chemical Process, Food Industry, Beverages, Oil & Gas, Pharmaceuticals
- Suction Type
- Positive Displacement
- Seals Type
- Mechanical Seal
- Priming
- Self-priming
- Pump Type
- Rotary Lobe
- Capacity
- 0.1 - 60 m3/hr
- Lobe Type
- Tri-lobe / Bi-lobe (as per requirement)
- Drive Type
- Electric Motor, Variable Frequency Drive Compatible
- Rotor Material
- SS316/SS304/EPDM Coated
- Surface Finish
- Mirror Polished (Food Grade)
- Max Solid Pass Through
- Up to 40 mm
- Direction of Rotation
- Bidirectional
- Weight
- Approx. 40 kg - 250 kg (depending on model)
- Seal Cooling
- Jacketed Seal Chamber (optional)
- Fluid Compatibility
- Suitable for Shear Sensitive and Viscous Fluids
- Serviceability
- Easy Disassembly for Maintenance
- Viscosity Range
- Up to 1,000,000 cP
- Shaft Coupling
- Flexible Coupling
Lobe Pump Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Units Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
Lobe Pump About
Experience crackerjack performance with our decorated Lobe Pump, engineered for valorous industrial demands. Featuring Tri-lobe or Bi-lobe design, mirror polished for food grade perfection, this pump handles viscosities up to 1,000,000 cP with ease. Equipped with robust SS316/SS304 rotors, flexible coupling, and an optional jacketed seal chamber, it's the best choice for hygienic, shear-sensitive, and viscous media. Try now to grab the best price for effortless, non-pulsating flow and bidirectional versatility-ideal for chemical, food, pharma, and oil & gas sectors.
Lobe Pump Applications and Competitive Advantages
Used as a primary solution for efficient fluid transfer, the lobe pump suits industries like food processing, beverages, pharmaceuticals, oil & gas, and chemicals. Its crackerjack build makes it ideal for both gentle and viscous fluid handling. The decorated hygienic design, reversible flow, and easy maintenance set it apart. With valorous performance in demanding sites, this pump ensures high reliability, minimal noise, and superb cleaning-serving every sector where precise fluid movement is critical.
Certifications, Supply Capabilities, and Secure Shipping
Our lobe pumps comply with ISO, CE, and GMP standards, guaranteeing top-tier quality. With a supply ability tailored for industrial needs, each unit is packaged with utmost care for safe handover and timely dispatching. Secure shipping options ensure every pump arrives in impeccable condition. Custom packaging solutions are available to meet diverse client requirements, elevating your experience from order to operational handover with remarkable efficiency and reliability.
Lobe Pump Applications and Competitive Advantages
Used as a primary solution for efficient fluid transfer, the lobe pump suits industries like food processing, beverages, pharmaceuticals, oil & gas, and chemicals. Its crackerjack build makes it ideal for both gentle and viscous fluid handling. The decorated hygienic design, reversible flow, and easy maintenance set it apart. With valorous performance in demanding sites, this pump ensures high reliability, minimal noise, and superb cleaning-serving every sector where precise fluid movement is critical.
Certifications, Supply Capabilities, and Secure Shipping
Our lobe pumps comply with ISO, CE, and GMP standards, guaranteeing top-tier quality. With a supply ability tailored for industrial needs, each unit is packaged with utmost care for safe handover and timely dispatching. Secure shipping options ensure every pump arrives in impeccable condition. Custom packaging solutions are available to meet diverse client requirements, elevating your experience from order to operational handover with remarkable efficiency and reliability.
FAQ's of Lobe Pump:
Q: How does the lobe pump handle shear-sensitive or viscous fluids?
A: Thanks to its non-pulsating, positive displacement design and high-performance rotors, the lobe pump can proficiently transfer shear-sensitive and viscous fluids. The mirror-polished, food-grade surfaces further promote gentle handling while maintaining product integrity.Q: What are the primary applications of this lobe pump?
A: This lobe pump is widely used in the food and beverage industry, pharmaceuticals, dairy, chemical processing, and oil & gas sectors, making it versatile for transferring diverse industrial fluids-including those that are thick, abrasive, or demand strict hygiene.Q: Where can I use this pump?
A: You can deploy this lobe pump at sites requiring sanitary solutions and efficient fluid handling-factories, production lines, chemical plants, and processing environments prioritizing hygiene, CIP/SIP, or reversible flow.Q: What are the key benefits of choosing this decorated lobe pump?
A: Key benefits include easy disassembly for maintenance, variable frequency drive compatibility, robust construction using SS316/SS304, self-priming, non-pulsating flow, reversible operation, and validated certifications for food and pharma use-with each pump crafted to deliver reliable, valorous performance.Q: How is the product packaged and shipped?
A: Every lobe pump is handover-ready, securely packaged in compliance with industrial standards, and dispatched through reliable logistics partners. Custom packaging is available for added protection, ensuring safe delivery at your site.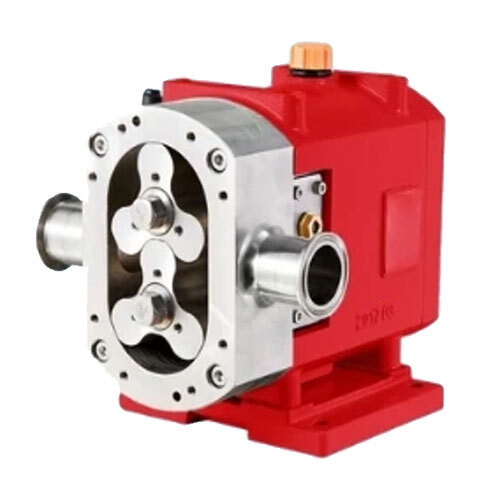
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Pump Category
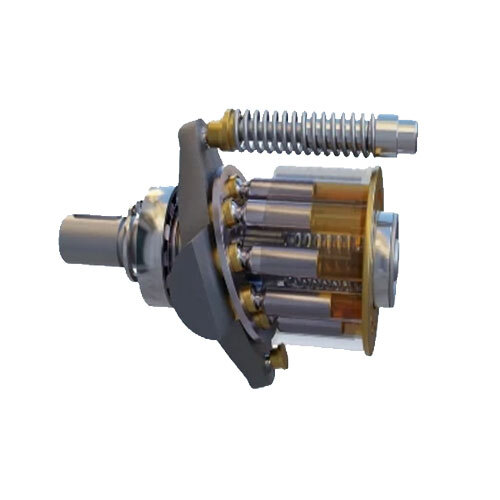
Dosing Pump
Minimum Order Quantity : 1 Unit
Pressure : Other, Up to 700 Bar (model dependent)
Usage : Other
Caliber : Customizable as per requirement
Pump Type : Other, Axial piston or radial piston pump
Frequency : 50 Hz/60 Hz (electric models)
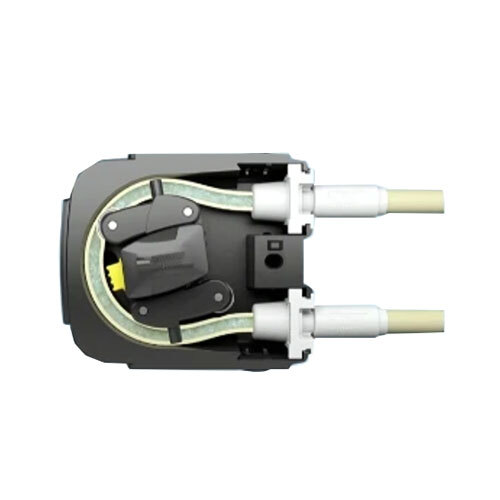
Peristaltic Pump
Minimum Order Quantity : 1 Unit
Pressure : Other, Max 2 bar (tubing and model dependent)
Usage : Other, Liquid transfer, dosing, sampling, laboratory, medical, and chemical processes
Caliber : 4 mm to 8 mm (based on tubing size)
Pump Type : Other, Peristaltic Hose Pump
Frequency : 50/60 Hz (AC models)
Jet Pump
Minimum Order Quantity : 1 Unit
Pressure : Medium Pressure
Usage : Other, Household, Agriculture, Water Transfer
Caliber : 25 mm
Pump Type : Other, Jet Pump
Frequency : 50 Hz
Mixed Flow Pump
Minimum Order Quantity : 1 Unit
Pressure : Other, Up to 2.5 MPa
Usage : Other, Water Supply, Industrial Process, Flood Control, Irrigation
Caliber : Customizable as per requirement
Pump Type : Other, Centrifugal, MixedFlow
Frequency : 50Hz / 60Hz

Contact Details
VISHWAARTH TECHNO-PROJECTS
GST : 24BFBPJ9269K1Z2
- B No I - 306, 3rd Floor, Dudheshwar Road,Ahmedabad - 380004, Gujarat, India
- Phone :08071724603
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
